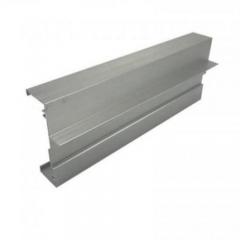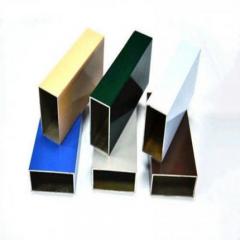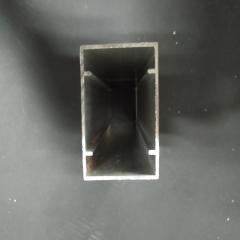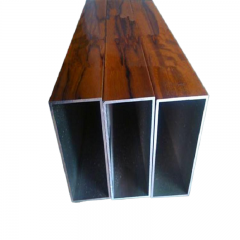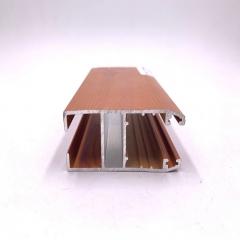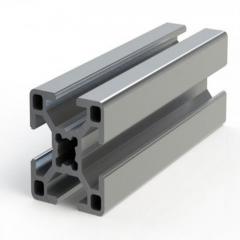
Have you ever wondered how those sleek window frames, elegant curtain walls, and intricate facade elements achieve such precise, consistent profiles? The answer lies in a remarkable manufacturing process that transforms raw metal into the building components shaping our modern skylines.
Architectural aluminum extrusions are specialized profiles created specifically for construction applications. Unlike generic aluminum products, these extrusions are engineered to meet the demanding performance, aesthetic, and durability requirements of contemporary architecture.
Imagine squeezing clay through a shaped opening—that's essentially how aluminum extrusion works, just with intense heat and tremendous pressure. The process begins with aluminum alloy billets, typically cut to lengths of 18 to 24 inches. These billets are heated to approximately 450°C to 500°C, reaching a plastic-like state where the metal becomes flexible while remaining solid.
At this temperature, the softened aluminum is forced through a steel die using powerful mechanical pressure. The die—a precisely machined tool—determines the exact cross-sectional shape of your final profile. Whether you need a complex curtain wall mullion or a simple window frame, the die shapes it all.
Once the heated aluminum exits the die, it undergoes rapid cooling using air or water to solidify its shape and enhance structural properties. But the process doesn't end there. The extruded aluminum is then stretched to relieve internal stresses and correct any slight distortions, ensuring perfectly straight profiles ready for architectural applications.
When discussing aluminum or aluminium (the spelling varies between American and British English), you're referring to the same remarkable material. The aluminium vs aluminum debate is purely linguistic—the extrusion process and material properties remain identical regardless of which term you prefer.
What sets architectural extrusions apart from industrial applications is the emphasis on precision tolerances, surface quality, and the ability to create profiles that integrate multiple functions into a single component.
Extruded aluminum has become the go-to material for architects and specifiers who demand both performance and design freedom. Unlike steel, which is typically formed by rolling, the aluminum extrusion process allows for virtually any cross-sectional shape—including intricate hollows, complex snap-fit features, and integrated channels.
Here are the key characteristics that make these extrusions indispensable for modern buildings:
This combination of properties allows architects to design truly bespoke profiles, moving beyond standard catalog shapes to achieve unique aesthetic visions while meeting strict performance criteria. The precision achievable through extrusion means components arrive on-site ready for installation, streamlining construction timelines and reducing on-site labor.
Sounds complex? Choosing the right aluminum alloy doesn't have to be. Think of it like selecting paint for a room—you need the right type for the specific job. For architectural aluminum extrusions, alloy selection directly impacts structural integrity, surface finish quality, and long-term performance of your building components.
The 6000-series aluminum alloys dominate architectural applications because they combine excellent extrudability with good mechanical properties. Among these, 6063, 6061, and 6005 emerge as the primary choices architects and engineers encounter when specifying profiles for construction projects.
When appearance matters most, 6063 aluminum is your ally. Often called the "architectural alloy," it delivers the smooth, consistent surfaces that decorative applications demand. Window frames, door systems, curtain wall mullions, and ornamental trim typically rely on this versatile material.
What makes 6063 special? Its chemical composition promotes exceptional flow during extrusion, allowing manufacturers to produce intricate profiles with sharp corners and fine details. The resulting surfaces accept anodizing beautifully, creating uniform color distribution and that premium finish clients expect.
According to mechanical property data from Engineering ToolBox, 6063-T6 offers a tensile strength of approximately 30,000 psi with a yield strength of 25,000 psi. While these numbers might seem modest compared to structural alloys, they're perfectly adequate for most non-load-bearing architectural elements.
Here's where the decision gets interesting. When your project involves load-bearing components—think structural frames, support brackets, or heavy-duty railings—aluminum 6061 steps into the spotlight.
So what is tensile strength, and why does it matter here? The tensile strength definition refers to the maximum stress a material can withstand while being stretched before breaking. For structural applications, higher tensile strength means greater load-carrying capacity and safety margins.
6061 aluminum delivers significantly higher mechanical properties. In the T6 temper condition, 6061 achieves tensile strength of 42,000 psi compared to 6063-T6's 30,000 psi—a 40% improvement. This makes a6061 material the preferred choice when structural reliability cannot be compromised.
However, this strength advantage comes with tradeoffs. 6061 produces slightly rougher surface finishes after extrusion, making it less ideal for visible decorative applications. The alloy also requires more aggressive machining parameters and may show less uniform coloring after anodizing.
Selecting between these alloys requires balancing multiple factors. Consider these questions when making your decision:
| Property | 6063-T6 | 6061-T6 | 6005-T5 |
|---|---|---|---|
| Tensile Strength (psi) | 30,000 | 42,000 | 38,000 |
| Yield Strength (psi) | 25,000 | 35,000 | 35,000 |
| Corrosion Resistance | Excellent | Good | Very Good |
| Surface Finish Quality | Excellent | Good | Very Good |
| Weldability | Excellent | Good | Good |
| Anodizing Response | Excellent | Fair | Good |
| Best Applications | Window frames, decorative trim, curtain walls | Structural components, load-bearing frames | Heavy-wall profiles, transit applications |
Notice the temper designations T5 and T6 in the table above. These indicate different heat treatment processes that significantly affect material properties. T5 temper means the aluminum was cooled from extrusion temperature and artificially aged—a simpler, more economical process. T6 temper involves solution heat treatment by artificial aging, producing higher strength but at increased cost.
For most architectural window and door applications, 6063-T5 provides sufficient strength while optimizing manufacturing efficiency. When structural calculations demand maximum performance, specifying T6 temper ensures you're getting the alloy's full potential.
Understanding these distinctions empowers you to write specifications that balance performance requirements with budget realities—a skill that separates experienced specifiers from novices.
When you walk into a supplier's catalog, the sheer variety of aluminum extrusion profiles can feel overwhelming. Angles, channels, tubes, bars—where do you even begin? Understanding the landscape of available shapes helps you make smarter specification decisions and opens doors to creative design solutions you might not have considered.
Architectural aluminum extrusions fall into two broad categories: standard off-the-shelf profiles and custom-engineered shapes. Each serves distinct purposes, and knowing when to leverage either approach can dramatically impact your project's budget, timeline, and design possibilities.
Standard profiles represent the workhorses of architectural construction. These readily available shapes ship quickly, cost less per foot, and require no upfront tooling investment. For many routine applications, they're exactly what you need.
Here's how standard architectural profiles break down by category:
Standard aluminum tube and channel sections are typically available in alloys 6061 and 6063, with wall thicknesses ranging from 1/16 inch to 1/4 inch. Lengths commonly run 12 to 24 feet, though suppliers often offer custom cutting services.
What happens when standard shapes can't achieve your design vision? Custom extrusion profiles step in. By developing a proprietary die, manufacturers can produce virtually any cross-sectional geometry you can imagine—integrating multiple functions into a single component.
Consider a curtain wall mullion that must incorporate:
No standard profile accomplishes all this. A custom extrusion consolidates these features into one piece, simplifying installation and improving system performance.
Die development involves upfront costs—typically ranging from a few hundred to several thousand dollars depending on complexity. However, for projects requiring significant quantities, this investment often pays back through reduced assembly labor, fewer components to inventory, and tighter quality control.
According to industry sources, today's engineers use advanced computer-aided design systems to develop complex die geometries while predicting material flow under pressure. This precision enables profiles with intricate details that would have been impossible just decades ago.
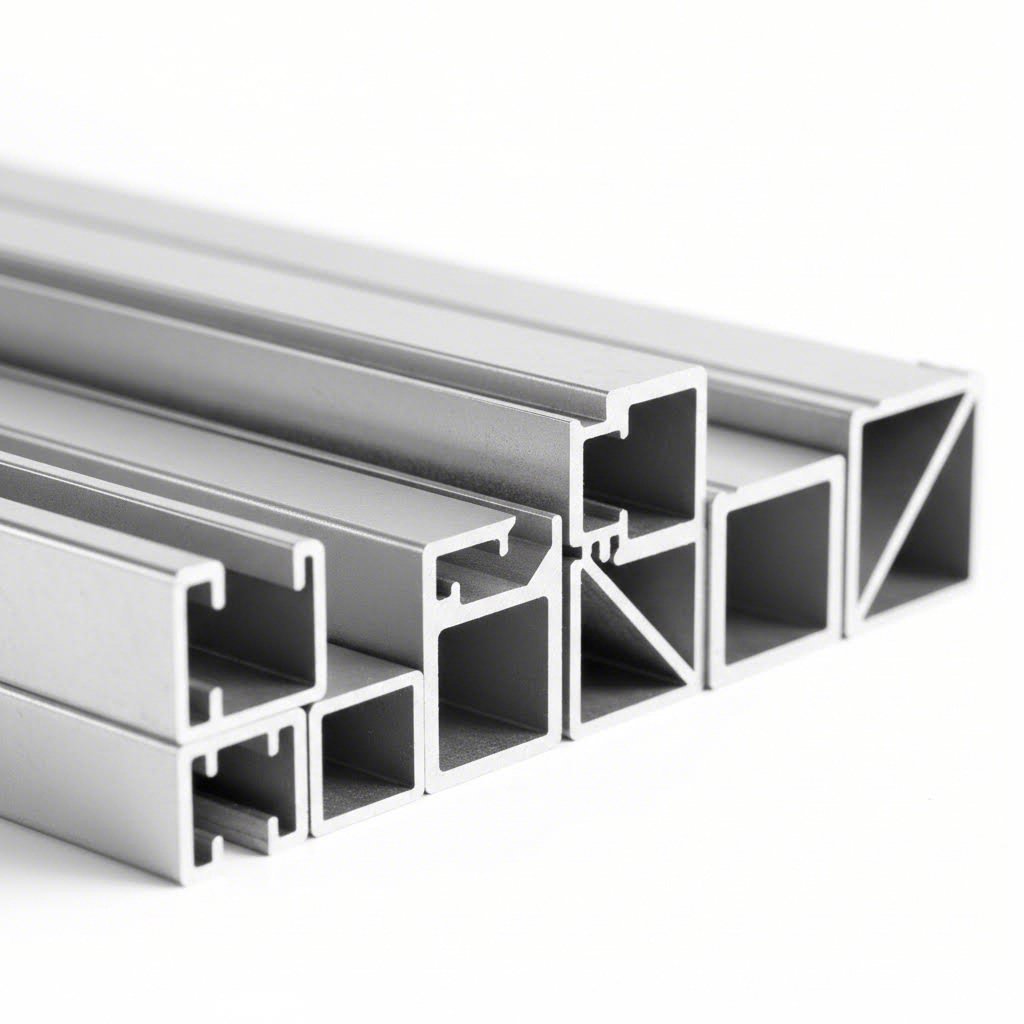
Understanding the distinction between hollow and solid extrusions matters for both structural and practical reasons. Solid profiles—like aluminum angle sections and flat bars—offer simplicity and maximum material strength at any given cross-section. They excel in applications requiring pure tensile or compressive loading.
Hollow profiles, including tubes and complex multi-void sections, provide superior bending resistance relative to their weight. A hollow rectangular tube can match the stiffness of a solid bar while weighing significantly less. This weight advantage translates to easier handling, lower shipping costs, and reduced dead loads on building structures.
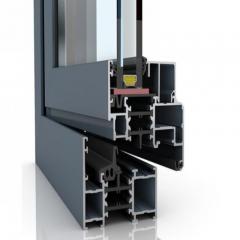
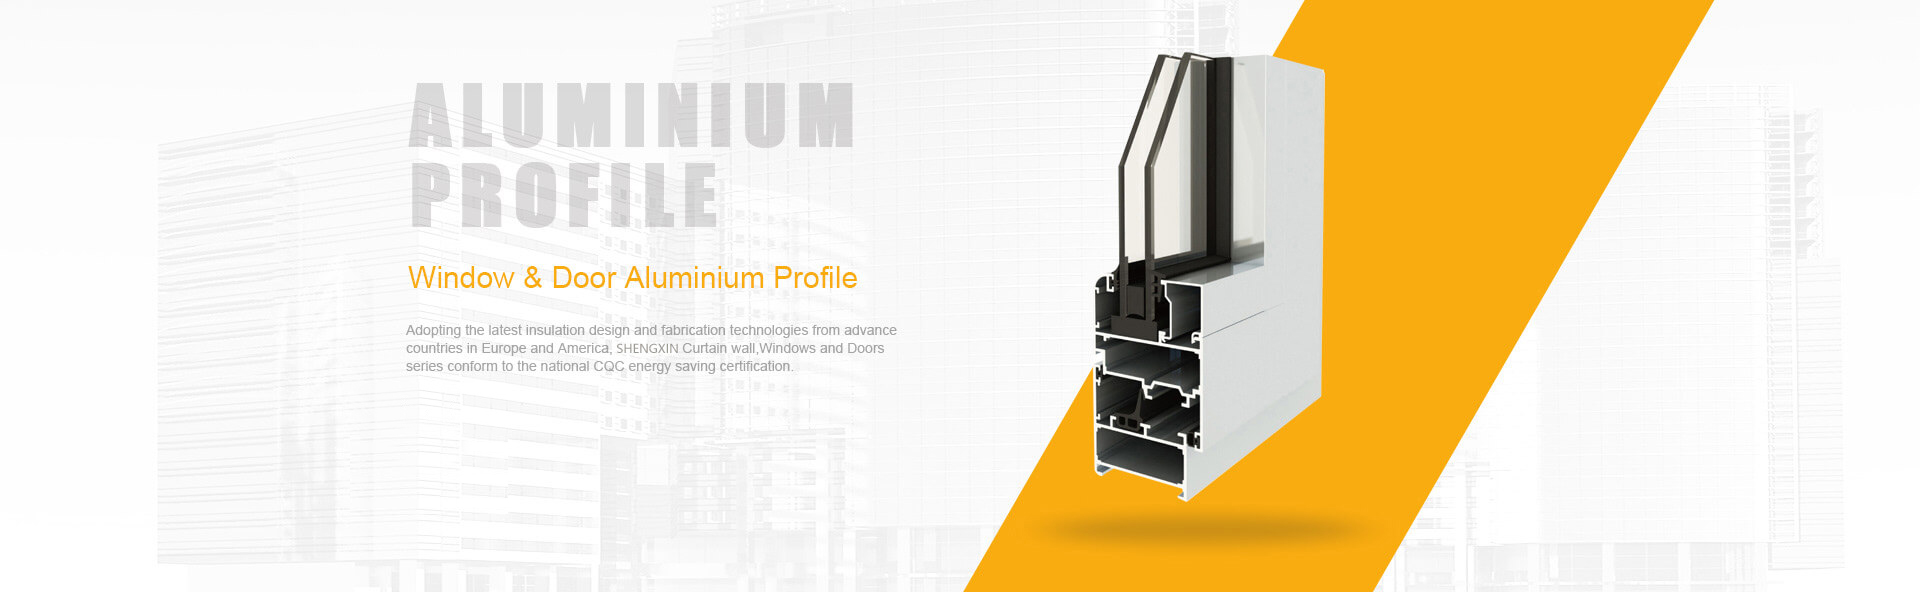
For architectural applications, hollow profiles also enable concealed fastening, internal wiring runs, and integration of thermal breaks. Window and door frames almost universally use hollow extrusions to accommodate weatherstripping, hardware, and insulating elements within the profile itself.
Tolerances become critical when profiles must fit together precisely. Standard extrusion tolerances typically range from ±0.008 inches to ±0.020 inches depending on profile size and complexity. For tight architectural fit-ups—such as corner miters on window frames or interlocking facade panels—specifying tighter tolerances may be necessary, though this can increase production costs.
With alloy selection and profile geometry now understood, the next consideration shaping your specification involves surface treatment—the finishes that protect your extrusions while defining their visual character.
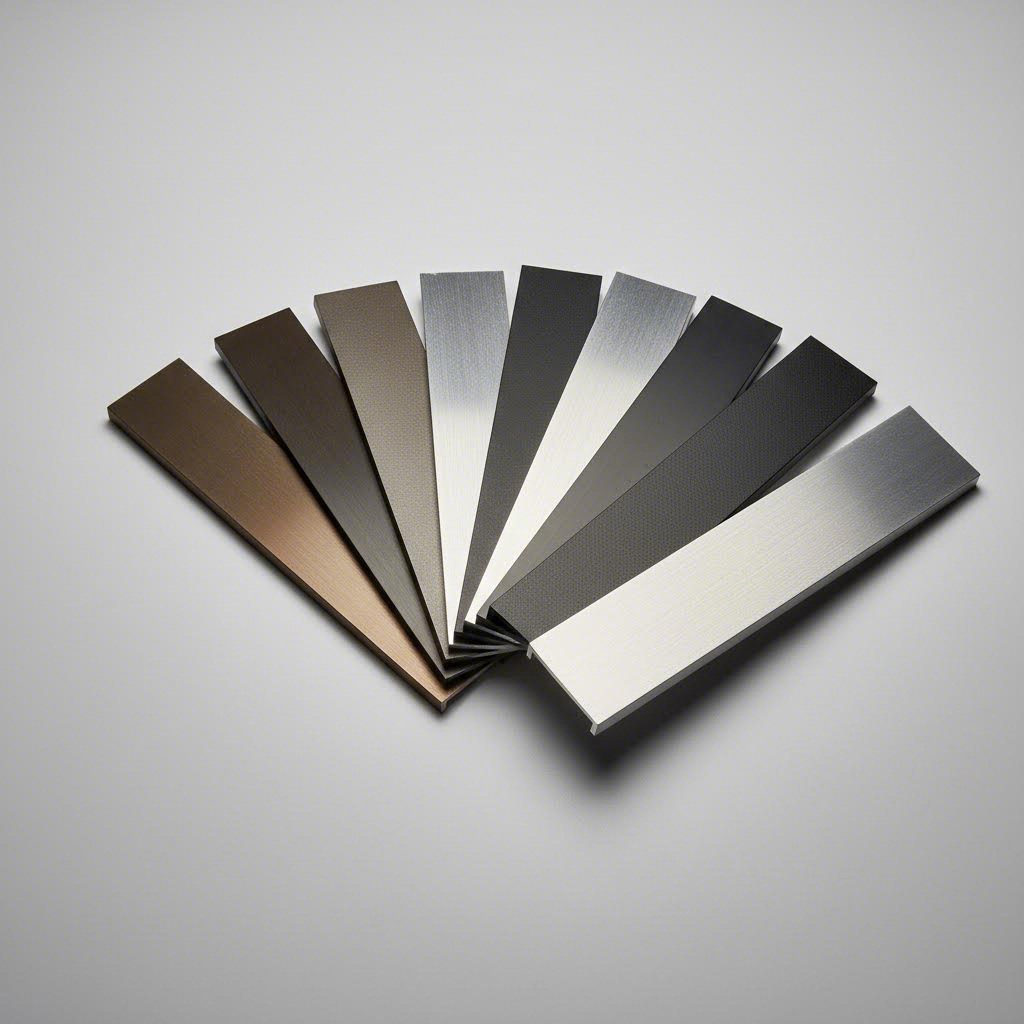
You've selected the perfect alloy and designed an ideal profile shape—but here's what truly brings architectural aluminum extrusions to life: the surface finish. This final layer determines whether your building components resist decades of weathering, match your design vision precisely, and maintain their beauty throughout the building's lifespan.
Choosing between anodizing, powder coating, and high-performance paint systems isn't merely an aesthetic decision. Each finish offers distinct performance characteristics, maintenance requirements, and cost implications that savvy specifiers must understand.
What exactly happens when aluminum becomes anodized? Unlike applied coatings that sit on top of the metal, anodizing transforms the aluminum surface itself through an electrochemical process. The result? A layer of aluminum oxide that's integral to the base metal—it cannot peel, flake, or chip like paint.
Here's how anodized aluminum achieves its remarkable durability: aluminum profiles are submerged in an acid electrolyte bath while electrical current passes through the solution. This process grows a protective oxide layer from the metal surface outward. The resulting coating features a honeycomb-like structure of microscopic pores that can absorb dyes for coloring before being sealed for permanence.
According to SAF finishing guidelines, coating thickness directly determines durability. The industry recognizes two primary classifications:
Anodized metal finishes range from clear (natural silver) to bronze, black, champagne, and custom architectural colors. The alu anodized look delivers a distinctive metallic luster that painted finishes simply cannot replicate—a translucent quality that reveals the aluminum's natural character while providing protection.
One often-overlooked advantage: anodizing is renewable. When an anodized surface appears weathered after years of exposure, mild abrasive cleaning can remove surface deposits and reveal fresh oxide beneath. This restoration capability extends service life significantly beyond most organic coatings.
Imagine paint without liquid solvents—that's essentially powder coating. Dry pigment particles encapsulated in powdered resin are electrostatically applied to aluminum surfaces, then cured in ovens where they melt and fuse into a continuous film.
Why has powder coating gained tremendous popularity for architectural applications? The environmental advantages are compelling. Powder coatings emit virtually no volatile organic compounds (VOCs) during application, making them increasingly attractive as environmental regulations tighten.
Modern AAMA 2605-certified powder coatings now offer 20 to 30-year warranties, placing them on par with premium paint systems. These advanced formulations, often based on FEVE or PVDF resins, deliver exceptional UV resistance and color stability that earlier powder technologies couldn't match.
Powder coating excels in specific scenarios:
However, powder coating presents challenges. Orange peel texture can occur if application parameters aren't precisely controlled. Color matching requires larger minimum orders than liquid paint. And touch-up repairs prove more difficult than with conventional coatings. For aluminum flat bar and simple profile shapes, these limitations rarely matter—but complex assemblies may benefit from liquid alternatives.
For the most demanding architectural applications—coastal environments, industrial zones, or buildings where 30+ year performance is non-negotiable—PVDF coatings represent the gold standard. Known commercially as Kynar 500 or Hylar 5000, polyvinylidene fluoride resins have protected curtain walls and metal roofing since 1965.
What makes PVDF exceptional? The molecular structure resists UV degradation and chemical attack better than virtually any other organic coating. Colors remain stable for decades, and the finish maintains its integrity in environments that would destroy lesser coatings.
AAMA 2605 specification requires actual 10-year South Florida exposure testing—real-world proof rather than accelerated laboratory simulations. As industry experts note, PVDF coatings have dominated the curtain wall and metal roofing markets because they deliver unmatched color consistency across large projects.
For extreme durability requirements beyond conventional finishes, micro-arc oxidation (MAO) offers another option. This plasma-based process creates ceramic-like oxide layers significantly harder and more wear-resistant than standard anodizing—though at considerably higher cost.
| Finish Type | Durability Rating | Color Options | Maintenance | Best Applications |
|---|---|---|---|---|
| Anodizing (Class I) | 20-40+ years | Clear, bronze, black, limited custom | Periodic cleaning; renewable surface | Storefronts, door systems, high-traffic areas |
| Anodizing (Class II) | 10-20 years | Same as Class I | Same as Class I | Interior trim, moderate exterior use |
| Powder Coating (AAMA 2604) | 10-15 years | Full RAL spectrum, textures | Annual washing recommended | General architectural, interior/exterior |
| Powder Coating (AAMA 2605) | 20-30 years | Wide range including metallics | Annual washing recommended | Premium curtain walls, facades |
| PVDF/Kynar (Liquid) | 30+ years | Virtually unlimited custom | Annual washing recommended | Curtain walls, metal roofing, harsh environments |
| Wood Grain/Specialty | 15-25 years | Realistic wood patterns, stone effects | Depends on base coating | Decorative applications, residential |
When specifying finishes, consider the building's exposure conditions, maintenance access, and design intent. An anodized aluminum material finish suits projects demanding that authentic metallic character. PVDF excels where color uniformity across large facades matters most. And powder coating offers the broadest aesthetic palette with strong environmental credentials.
Surface treatment decisions made today will define your building's appearance for decades—making this specification choice one of the most consequential in the entire project.
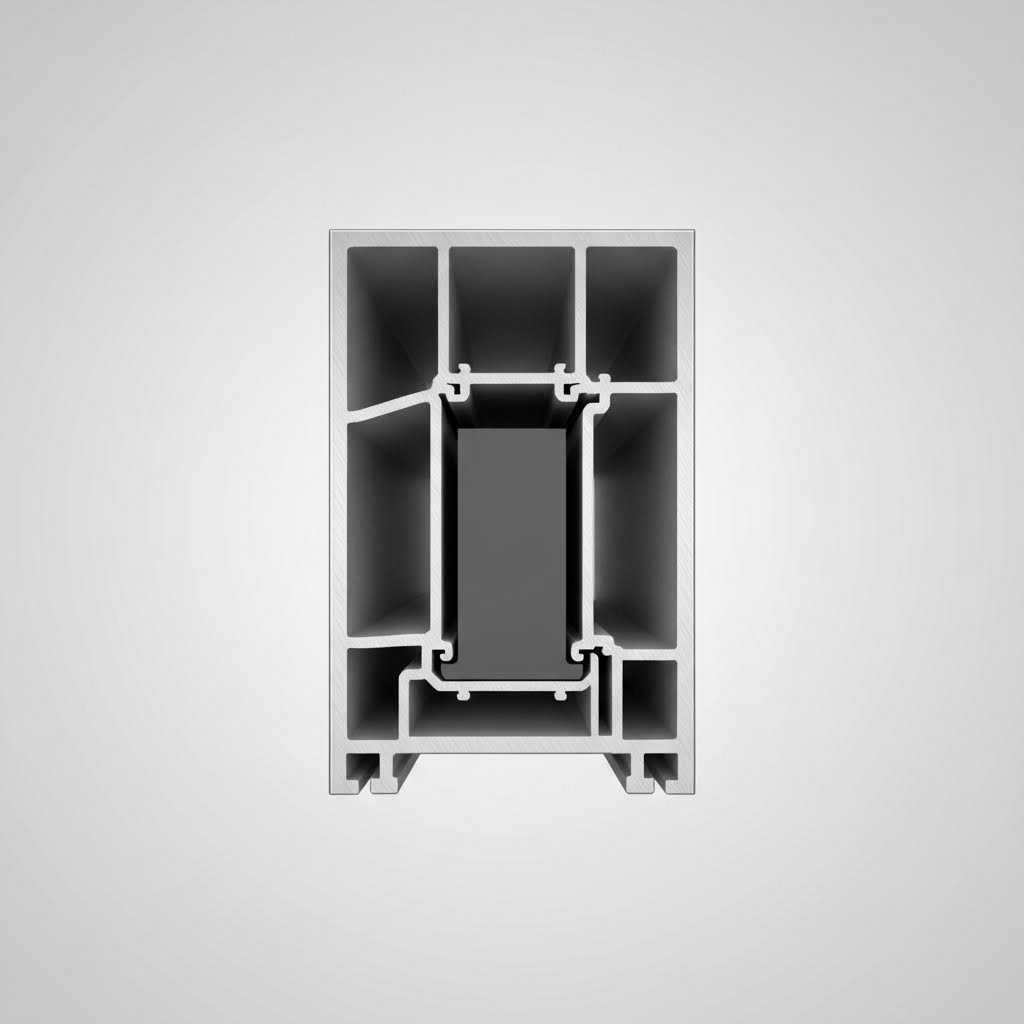
Here's a secret many architects learn the hard way: specifying beautiful aluminum profiles means nothing if your building envelope hemorrhages energy. Without proper thermal management, those sleek aluminum frame systems become expensive thermal bridges—conducting heat straight through your carefully designed facade.
What is aluminum at its core? An exceptional conductor. While this property makes aluminum ideal for heat sinks and cookware, it creates challenges for building envelopes where thermal separation matters. This is precisely where thermal break technology transforms architectural aluminum extrusions from energy liabilities into high-performance building components.
Imagine a bridge connecting two cities—now imagine cutting that bridge in half with an insulating barrier. That's essentially what a thermal break does within an aluminum profile. These non-conductive barriers interrupt the direct path heat would otherwise travel through the metal.
Modern thermal break systems typically use polyamide (nylon) strips or struts positioned between interior and exterior aluminum sections. According to Technoform's technical documentation, these high-precision insulating profiles can reduce energy loss by up to 85%—a staggering improvement that translates directly into lower operating costs and reduced carbon emissions.
The polyamide barrier concept works through a simple principle: materials with low thermal conductivity placed between conductive aluminum sections dramatically slow heat transfer. Traditional thermal breaks measure approximately 0.25 to 0.375 inches thick, though advanced systems now offer dual breaks and extended depths approaching one inch or more for superior performance.
Beyond energy savings, thermal breaks deliver critical moisture control. When warm interior air meets cold exterior surfaces, condensation forms. In non-thermally broken aluminum frames, this moisture can damage finishes, promote mold growth, and compromise adjacent building materials. Properly designed thermal barriers keep interior aluminum surfaces warm enough to prevent condensation under normal operating conditions.
Energy codes have tightened dramatically over the past decade, making thermal performance a specification requirement rather than an optional upgrade. The 2015 International Energy Conservation Code requires maximum U-factors of 0.38 Btu/ft²·°F·hr for fixed fenestrations in Climate Zone 5—a threshold that traditional aluminum curtain walls without thermal improvements simply cannot meet.
Understanding what these numbers mean helps you specify correctly. U-factor measures the rate of heat transfer through an assembly—lower values indicate better insulating performance. Traditional aluminum-framed curtain walls with basic thermal breaks typically achieve U-factors between 0.45 and 0.6. High-performance systems with advanced thermal break technology can approach 0.3 or better.
The tensile breaking strength of thermal break components matters for structural integrity. Polyamide struts must maintain their mechanical properties under sustained loading while the aluminum profile resists wind forces and dead loads. Quality manufacturers engineer their thermal break systems to handle these combined stresses without compromising either thermal or structural performance.
Here's why thermal performance impacts sustainable building certifications:
Specifying thermal performance requires understanding how manufacturers calculate and report their numbers. Whole-assembly U-factors combine the performance of framing, glazing, and their interactions—a more meaningful metric than component-level values considered in isolation.
Several thermal enhancement strategies can stack together for cumulative improvement. According to building enclosure consultants Simpson Gumpertz & Heger, options include:
When evaluating aluminum profile systems with thermal breaks, request project-specific thermal calculations that account for your actual glazing selections and frame configurations. Generic catalog values may not reflect installed performance in your specific application.
For aluminum decking and other exterior applications where thermal bridging through the building envelope occurs, similar principles apply. Continuous insulation strategies and thermal isolation details at attachment points prevent these elements from short-circuiting your wall assembly's insulation.
The lifecycle implications extend beyond operating costs. Buildings designed with high-performance thermal envelopes command premium rents, maintain value better during resales, and avoid costly retrofit requirements as energy codes continue tightening. Specifying thermally broken aluminum systems today positions your projects for decades of regulatory compliance and market competitiveness.
Now that you understand alloys, profiles, finishes, and thermal performance—how do you actually specify architectural aluminum extrusions for real projects? This is where theory meets practice. Different building types demand different approaches, and knowing how to match specifications to project requirements separates experienced specifiers from those still learning the craft.
From towering curtain walls to intimate residential windows, aluminum extrusions serve remarkably diverse applications. Each demands specific performance criteria, structural considerations, and installation details that influence your specification decisions.
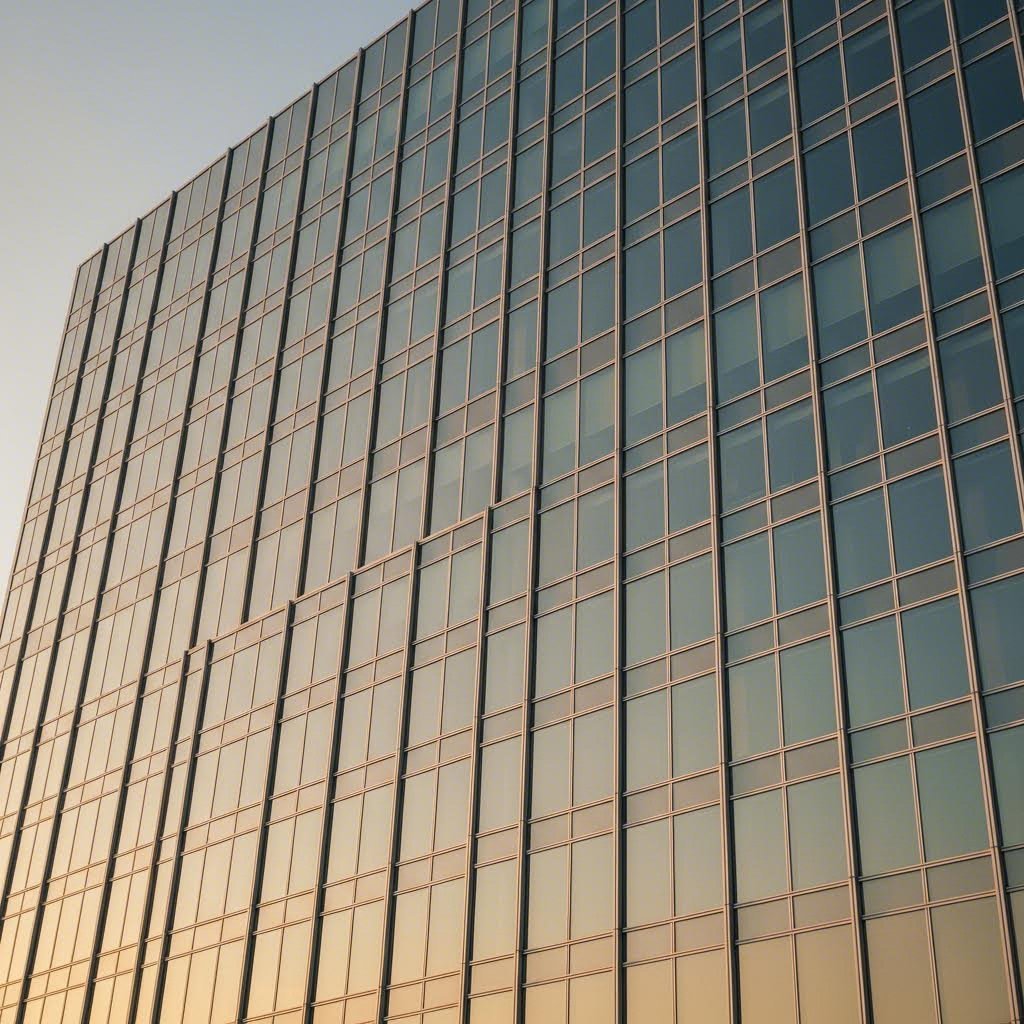
Commercial facades represent the most demanding application for architectural aluminum extrusions. These systems must resist wind loads, manage water infiltration, accommodate building movement, and maintain thermal performance—all while delivering the aesthetic vision your design intends.
When specifying curtain wall mullions and transoms, consider these critical requirements:
For very tall facades, aluminum tubing and reinforced mullion profiles may incorporate internal stiffeners where standard extrusions would exceed deflection limits. Typical glazing-deflection acceptance ranges from L/175 to L/240 depending on glass type—specify this limit clearly in contract documents.
Unitized curtain wall systems—where large pre-glazed units are assembled in factory-controlled settings—often outperform stick-built approaches for complex geometries and high-rise applications. Factory tolerances typically range from ±1.5 mm to ±3 mm depending on complexity, enabling tighter quality control than field assembly allows.
Residential and light commercial window systems present different specification challenges. Here, thermal performance, hardware integration, and operational reliability take precedence over the extreme structural demands of curtain walls.
According to aluminum window profile manufacturers, wall thickness requirements vary by configuration. Outward-opening windows should have profiles no less than 1.8mm thick, while inward-opening designs can use minimum 1.4mm material. For windows exceeding 3-4 square meters, consider increasing profile thickness or adding intermediate posts for enhanced physical strength.
Aluminum trim profiles surrounding windows serve both aesthetic and functional purposes:
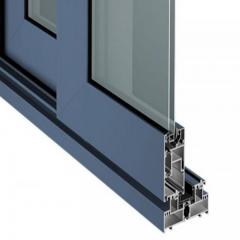
Sliding door track systems demand particular attention to load-bearing capacity and smooth operation. Heavy glass panels require robust aluminum track extrusions with proper roller systems. Specify track profiles that accommodate weather seals, drainage channels, and threshold transitions while maintaining low-friction operation.
For storefronts and commercial entries, aluminum awning systems extend building protection while creating visual interest. These applications combine structural aluminum framing with glazing or solid panels, requiring careful attention to attachment details and water management at transitions.
Inside the building envelope, aluminum extrusions serve equally important—though less demanding—applications. Interior trim, partition systems, and decorative elements benefit from aluminum's precision, durability, and design flexibility.
Common interior applications include:
Interior applications typically specify 6063 alloy for superior surface finish quality, with Class II anodizing or powder coating providing adequate protection for indoor environments. Without exposure to UV radiation and weather, interior finishes maintain appearance with minimal maintenance.
Aluminum decking, railings, and site furnishings extend the material's application beyond the building envelope. These exposed elements face direct weathering, requiring careful specification of alloys and finishes appropriate for outdoor service.
For aluminum decking systems, consider:
Exterior railings and site elements typically use 6061 or 6063 alloys with Class I anodizing or AAMA 2605-compliant coatings for maximum weather resistance. In coastal environments, specify enhanced corrosion protection and consider profile designs that shed water rather than trapping moisture.
With application requirements now clear, the next critical step involves navigating the specification process itself—from initial design through fabrication and delivery.
You've identified the perfect alloy, designed an ideal profile, and selected a durable finish—but how does your concept actually become a physical aluminum extrusion ready for installation? This journey from design intent to delivered product involves multiple stakeholders, critical decision points, and timeline considerations that experienced specifiers navigate with confidence.
Understanding the complete specification process prevents costly surprises and schedule delays. Whether you're ordering stock aluminum extrusion profiles or commissioning custom shapes, knowing what to expect at each stage empowers you to plan realistically and communicate effectively with manufacturing partners.
The specification journey begins with a critical choice: stock profiles or custom extrusions? This decision shapes everything that follows—from timeline and budget to design flexibility and minimum order quantities.
Stock profiles offer compelling advantages for straightforward applications. Standard aluminum bar stock, channels, and tubes ship from inventory within days, require no tooling investment, and often carry lower per-foot costs due to production efficiencies. When a standard shape meets your requirements, there's rarely reason to pursue custom alternatives.
However, custom aluminum extrusions unlock design possibilities stock shapes cannot match. According to industry manufacturing experts, the custom extrusion process begins with an in-depth consultation to understand requirements including desired shape, dimensions, mechanical properties, and end-use applications.
Here's what typically happens during initial supplier engagement:
Effective communication during this phase prevents misunderstandings later. Provide complete drawings with tolerances, specify alloy and temper requirements clearly, and communicate your quality expectations upfront. The more information suppliers receive initially, the more accurate their proposals will be.
For custom profiles, die development represents the most significant upfront investment and timeline driver. The extrusion die—a precision-machined steel tool that shapes aluminum as it's extruded—must be manufactured to exact specifications before production can begin.
Die complexity directly impacts both cost and lead time. Simple solid profiles with basic geometry might require dies costing $500 to $1,500, while complex hollow sections with tight tolerances can reach $3,000 to $8,000 or more. As manufacturing references indicate, designing the die requires precision and expertise because even minor errors can affect the final product's dimensions and quality.
Typical timeline expectations for custom aluminum extrusions include:
Total lead times for custom extruded aluminium profiles typically range from 8 to 14 weeks, though expedited timelines are sometimes possible at premium pricing. Stock aluminum bar and standard profiles ship much faster—often within days to two weeks.
Before committing to production quantities, most projects require sample approval. Initial prototypes serve as proof of concept, allowing evaluation of the extrusion's design and functionality. Any issues identified during testing are addressed through die modifications before full-scale production begins.
Quality control separates reliable architectural aluminum extrusions from problematic ones. Understanding inspection criteria and documentation requirements helps you specify appropriately and evaluate supplier capabilities.
Dimensional accuracy represents the first quality checkpoint. Standard extrusion tolerances follow industry specifications like ANSI H35.2, but architectural applications often demand tighter control. Specify your tolerance requirements clearly—typical architectural tolerances range from ±0.008 inches for critical dimensions to ±0.020 inches for less critical features.
Quality assurance programs should address:
For critical structural applications, request material certifications documenting alloy composition and temper. These mill certificates provide traceability and verify that the aluminum bar stock or billet used meets specified alloy requirements.
Surface finish inspections become particularly important for visible architectural elements. Anodizing thickness, powder coating adhesion, and color consistency should be verified before shipping. Many suppliers offer sample panels for finish approval before coating full production quantities.
Establishing clear inspection criteria and approval processes before production begins prevents disputes and ensures delivered extrusions meet your project's requirements.
Minimum order quantities vary significantly between suppliers and profile types. Stock profiles may ship in single pieces, while custom extrusions typically require minimums ranging from 500 to 2,000 pounds depending on complexity and supplier policies. For small projects requiring custom profiles, consider whether the design could be modified to use standard shapes, or whether higher per-piece costs for small runs still make economic sense.
With specification fundamentals established, the next consideration involves selecting a manufacturing partner with capabilities aligned to your project's specific requirements.
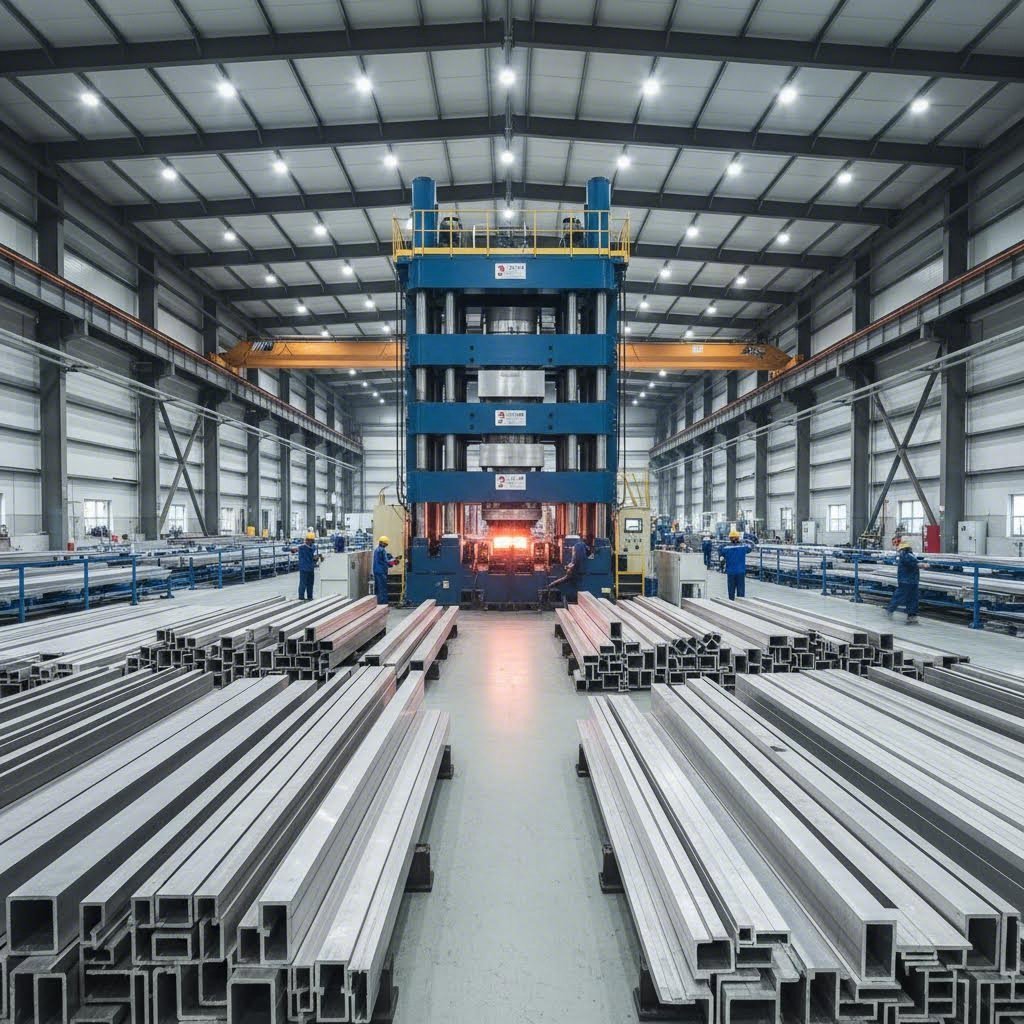
You've invested considerable effort developing the perfect profile specification—but here's a reality many architects discover too late: your manufacturing partner determines whether that specification becomes a flawless building component or a frustrating compromise. Not all extrusion suppliers possess equal capabilities, and mismatched partnerships lead to missed deadlines, quality issues, and costly project delays.
Selecting the right manufacturing partner requires evaluating technical capabilities, quality systems, and service depth. Whether you need standard aluminum channel profiles or complex custom shapes, understanding what distinguishes capable suppliers from marginal ones protects your project from preventable problems.
The extrusion press defines what profiles a supplier can actually produce. Think of press tonnage like an engine's horsepower—it determines what loads the equipment can handle and what profile sizes become possible.
According to industry evaluation guidelines, press capacity categories serve different purposes:
Why does this matter for your project? A supplier with multiple press capacities can handle diverse profile requirements and maintain flexibility when production volumes change. If your project includes both delicate decorative trim and substantial structural members, you'll need a partner whose equipment range spans these requirements.
For example, manufacturers like Shengxin Aluminium operate 35 extrusion presses ranging from 600T to 5500T, providing the versatility to produce everything from intricate aluminum strut channel profiles to heavy-duty structural sections within a single facility. This breadth of capability simplifies procurement and ensures consistent quality across diverse profile types.
Beyond press tonnage, evaluate alloy management practices. Reliable suppliers maintain controlled billet inventory across multiple alloy grades and verify homogenization and preheating processes—factors that directly impact extrusion consistency and surface quality.
Raw extrusions rarely arrive job-site ready. Most architectural applications require secondary operations—cutting, drilling, machining, surface treatment—that transform profiles into installation-ready components. Suppliers offering integrated deep processing services deliver significant advantages over those providing only basic extrusion.
CNC machining capabilities deserve particular scrutiny. According to manufacturing capability assessments, sophisticated facilities offer multiple machining center types including double-pallet VMCs, large-bed gantry CNCs with work envelopes up to 12 feet, and specialized tube laser systems. These capabilities enable precise cutting, drilling, milling, and complex fabrication that field operations simply cannot match.
Consider what value-added services your project requires:
Surface treatment integration provides another critical advantage. When extrusion, machining, and finishing occur under one roof, batch consistency improves dramatically. A profile requiring anodizing and drilling maintains dimensional and color uniformity when processed completely within a single facility—eliminating the quality variations that occur when components travel between subcontractors.
Comprehensive manufacturers offer extensive finishing options including anodizing in custom colors like champagne and rose gold, powder coating across the full RAL spectrum, PVDF coatings for maximum durability, and specialized processes like micro-arc oxidation for extreme wear resistance. This breadth enables single-source procurement regardless of your finish specification.
Beyond standard profiles, some applications require modular framing solutions. Systems like 8020 extrusion and aluminum unistrut provide standardized structural components for industrial and architectural applications. Suppliers familiar with these systems can advise on compatibility and provide matching accessories.
Evaluating manufacturing partners requires more than reviewing equipment lists. The right questions reveal whether a supplier's capabilities align with your project's specific demands—and whether their organization can support your needs beyond basic production.
Start with these essential evaluation criteria:
According to procurement best practices, strong technical communication differentiates professional suppliers from simple traders. Capable manufacturers provide design-for-manufacturability feedback on drawings, offer feasibility and cost optimization suggestions, and share inspection documentation before shipment.
Ask specifically about quality control systems:
Lead time reliability often proves the most practical indicator of capability. Request typical benchmarks: die manufacturing (10-20 days), extrusion production (7-15 days), and surface finishing (5-10 days). Ask how they manage production scheduling during peak seasons and whether ERP-based systems govern their planning.
For projects requiring display or mounting applications, inquire about specialty profiles like snap frame systems for signage and graphics. Suppliers experienced with these applications understand the precise tolerances and surface quality these visible components demand.
Finally, evaluate communication responsiveness. How quickly do they return inquiries? Do they proactively identify potential issues, or simply react after problems occur? Manufacturing partners who invest in relationship-building typically deliver more reliable outcomes than those focused purely on transactions.
The best manufacturing partnerships combine technical capability with collaborative communication—suppliers who function as problem-solving allies rather than order-takers.
With over 30 years of industry experience, established manufacturers like Shengxin Aluminium demonstrate how comprehensive capabilities—from die development through mass production—create value for architects and specifiers seeking reliable custom aluminum solutions. Their factory-direct model eliminates intermediary markups while providing end-to-end technical support throughout the specification journey.
Armed with these evaluation criteria, you're prepared to identify manufacturing partners whose capabilities match your project requirements—setting the stage for successful outcomes that begin at specification and extend through decades of building performance.
You've now explored the specification secrets that separate successful architectural aluminum projects from problematic ones—from alloy selection and profile design to thermal performance and manufacturing partnerships. But here's the bigger picture: choosing architectural aluminum means participating in one of construction's most sustainable material cycles while positioning your projects for decades of reliable performance.
As building codes tighten and sustainability expectations rise, understanding the lifecycle advantages of aluminum architecture becomes increasingly valuable. Let's examine why this material continues gaining favor among forward-thinking architects and specifiers.
What makes aluminum truly exceptional among building materials? Its infinite recyclability without property degradation. Unlike plastics that degrade with each recycling cycle or wood that eventually decomposes, aluminum maintains its structural and aesthetic properties through endless recycling loops.
Aluminum is an exception to the linear economy model, with its infinite recyclability without loss of quality. In a world economy that is only 7% circular, 75% of aluminum ever produced is still in use today.
According to Kawneer's sustainability research, creating recycled aluminum requires only 5% of the energy needed to produce new aluminum—a 95% energy reduction that translates directly into dramatically lower carbon emissions. This efficiency makes recycled aluminum one of the most environmentally responsible material choices available to architects.
The uses of the element aluminum extend far beyond initial construction. When buildings eventually reach end-of-life, extracted aluminum retains known economic value and enters established recycling infrastructure. Unlike materials that become landfill waste, architectural aluminium components return to the material stream, becoming new billets for future projects.
Modern manufacturers have embraced closed-loop recycling systems. Process scrap from extrusion operations returns to billet cast-houses for reuse in new production. This circular approach, combined with sourcing primary aluminum from clean energy smelters, enables low-carbon offerings with footprints more than 60% lower than industry averages.
Architectural aluminum continues evolving to meet changing demands. According to industry trend analysis, several developments are reshaping how architects specify and apply extruded profiles:
The modular construction sector—projected to reach $189 billion by 2032—increasingly relies on aluminum's lightweight durability for prefabricated exterior panels. These systems reduce site waste by 30-50% while maintaining consistent quality across multi-site projects.
Green building demands are also driving innovation. Renewable-powered electrolysis has reduced aluminum production emissions by 60%, with hydrogen-based smelting eliminating direct CO₂ emissions in pilot facilities. These advances support the industry's goal to decarbonize 37% of electricity-related emissions by 2030.
Companies like coast aluminum & architectural and specialized manufacturers continue pushing material capabilities forward, ensuring architects have access to profiles that meet increasingly demanding performance and aesthetic requirements.
Armed with the specification knowledge from this guide, you're prepared to leverage architectural aluminum extrusions more effectively than ever. Here's a quick summary of the key selection criteria covered:
For architects and specifiers seeking custom 6063 aluminum solutions, architectural window frames, or complex industrial profiles, working with experienced manufacturers provides end-to-end support from die development to mass production. With over 30 years of industry experience, Shengxin Aluminium offers factory-direct pricing and comprehensive capabilities—from their 35 extrusion presses to advanced CNC machining and surface treatment options including custom-color anodizing, powder coating, PVDF, and micro-arc oxidation.
Ready to explore what's possible for your next project? Visit Shengxin Aluminium's custom extrusion services to discuss your requirements with their technical team and discover how precision-engineered profiles can elevate your architectural vision.
What is anodized aluminum's role in your next facade? How might thermally broken profiles transform your building's energy performance? The answers begin with a conversation—and the specification knowledge you now possess ensures that conversation starts from a position of confidence.
Architectural aluminum extrusions are specialized profiles engineered for construction applications including curtain walls, window frames, door systems, facade elements, storefronts, interior trim, and railings. They offer design flexibility, excellent strength-to-weight ratio, corrosion resistance, and recyclability. Custom profiles can integrate multiple functions—such as glazing pockets, thermal breaks, and drainage channels—into a single component, simplifying installation and improving building performance.
6063 aluminum is the preferred 'architectural alloy' for decorative applications due to its superior surface finish and excellent anodizing response—ideal for window frames and visible trim. 6061 aluminum offers approximately 40% higher tensile strength (42,000 psi vs 30,000 psi in T6 temper), making it better suited for structural, load-bearing components. Choose 6063 when appearance matters most; specify 6061 when structural performance is critical.
Custom aluminum extrusion lead times typically range from 8 to 14 weeks total. This includes die design and engineering (1-2 weeks), die manufacturing (2-4 weeks), sample extrusion and approval (1-2 weeks), production runs (2-4 weeks), and surface finishing (1-2 weeks). Stock profiles ship much faster—often within days to two weeks. Expedited timelines may be available at premium pricing from manufacturers with comprehensive in-house capabilities.
Major finish options include anodizing (Class I and II in clear, bronze, black, and custom colors), powder coating (thousands of RAL colors with AAMA 2604 or 2605 certifications), PVDF/Kynar coatings for 30+ year durability, and specialty finishes like wood grain patterns. Anodizing creates an integral oxide layer that cannot peel, while PVDF coatings offer maximum color stability for demanding exterior applications. Surface treatment selection depends on exposure conditions, aesthetic requirements, and maintenance expectations.
Thermal breaks are non-conductive polyamide barriers positioned between interior and exterior aluminum sections that can reduce energy loss by up to 85%. Without them, aluminum's high thermal conductivity creates thermal bridges that waste energy and cause condensation. Thermally broken profiles help meet stringent energy codes, reduce HVAC loads, prevent moisture damage, improve occupant comfort, and support sustainable building certifications like LEED.


 serviço on-line
 0086 136 3563 2360
 sales@sxalu.com
 +86 136 3563 2360
 português
 English
 français
 Deutsch
 русский
 español
 العربية
 ไทย
 Việt
 Українська